
Introduction: A Question from the Shop Floor
Have you noticed how a single solder line can change the mood of an entire assembly room? In my visits to small PCB shops and large manufacturing halls, I repeatedly see the same scene: operators clustered near reflow lanes, masked or not, while vents hum in the background. Fume extraction for electronics and industrial applications shows up in this second sentence because the problem is not abstract — it is the air they breathe every shift. Recent field surveys suggest that many facilities report elevated particulate and VOC counts during peak runs (some sites record spikes lasting minutes to hours), so the data is clear enough to make one ask: are we solving the right problem or only treating symptoms? I bring this up with academic tone but also as someone who spends time on the floor — I care. This piece will move from the observable scene to deeper issues, and then look ahead to practical choices you can make next.
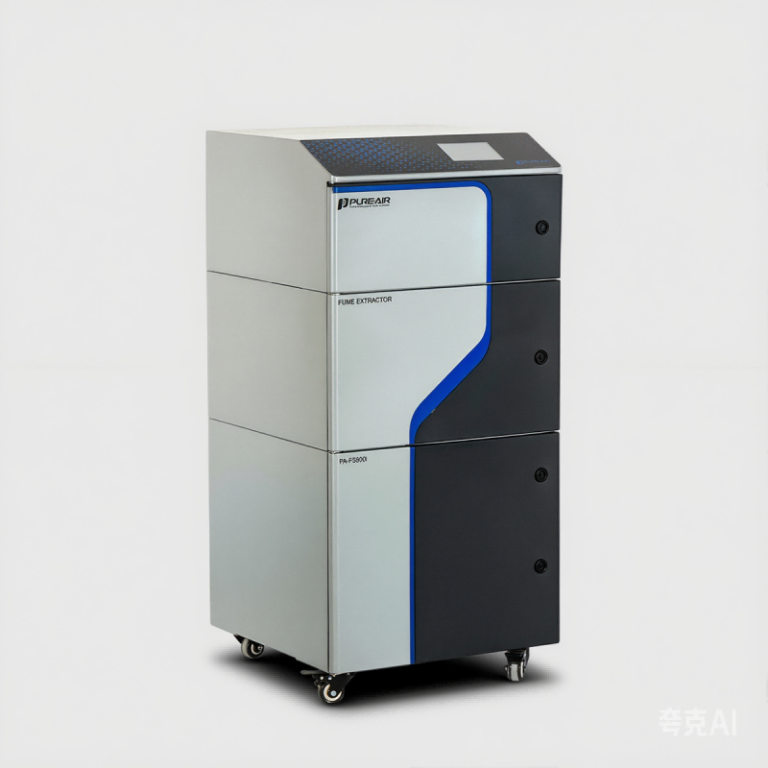
Part 2 — Unseen Fault Lines in Reflow Soldering Ventilation
What breaks down in current set-ups?
I want to start direct: reflow soldering is at the heart of modern PCB assembly, but many extraction systems were not designed for its dynamic emissions profile. In practice, filtration units and canopy hoods struggle with pulses of condensable flux vapors and fine particulates produced during lead-free cycles. The result is uneven capture efficiency and frequent filter loading — and yes, maintenance windows become crises. From my observations, common faults include poor hood placement, mismatched airflow rates, and reliance on one-size-fits-all filters (HEPA plus carbon is common, but sometimes inadequate for specific VOC mixes). Industry terms here matter: volatile organic compounds, particulate matter, and downflow versus crossflow dynamics all play roles. Look, it’s simpler than you think to miss this — operators focus on throughput, managers focus on uptime, and air quality drifts downhill between them.
Technically speaking, the transient thermal gradients in reflow zones create short-lived plumes that carry heavy condensates. Edge phenomena — like localized backflow when conveyor speed changes — defeat static capture models. Power converters and nearby heating elements can alter local air currents. If you want to tighten control, you must consider plume modeling and real-time sensor feedback, not just larger fans. I recommend integrating simple particle monitors and targeted capture hoods; they reveal patterns you would otherwise never see. And oh — maintenance scheduling must move from reactive to planned, with filter differential pressure checks and pre-emptive carbon replacement. This is not glamorous, but it works.
Part 3 — Principles for Better Systems and How to Choose Them
What’s Next for Cleaner Lines?
Moving forward, I favor a principles-first approach. For new installations around reflow soldering, design from the plume outward: model the thermal plume, select a hood geometry that intercepts the plume at its strongest point, then size the capture fan and filtration for the expected VOC load and particulate burst. This means combining CFD-informed placement with modular filtration stacks — combining HEPA, activated carbon, and sometimes catalytic stages for specific chemistries. Short sentences: test early. Long ones: iterate with small adjustments, measure, and adjust again — funny how that works, right?
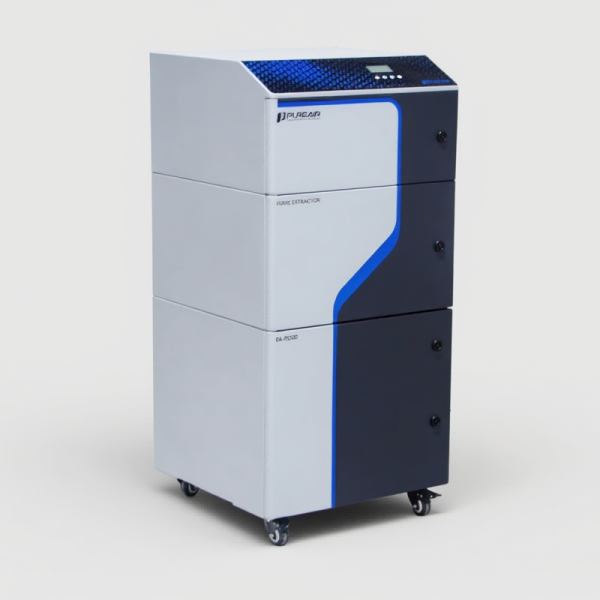
I also advise embracing smarter maintenance and monitoring. Install continuous particle counters and VOC sensors, tie them to simple alarms, and log trends. Edge computing nodes can process this stream locally and trigger incremental fan speed changes, preserving filter life and energy. From a practical stance, you want systems that are service-friendly: quick-change filter cartridges, clear access panels, and documented replacement intervals. And remember: training people to read differential pressure and simple sensor outputs pays dividends every month. — small investment, big returns.
To close with a brief advisory, here are three metrics I use when comparing systems: 1) Capture Efficiency at the plume source (measured for your process), 2) Filter Lifecycle Cost (including disposal and downtime), and 3) Response Latency of monitoring and control (how fast the system reacts to a spike). Evaluate these, and you will choose systems that protect workers and production alike. I’ve tested setups on real lines and seen the difference. For practical solutions and more tools, see PURE-AIR.